SPIRALS
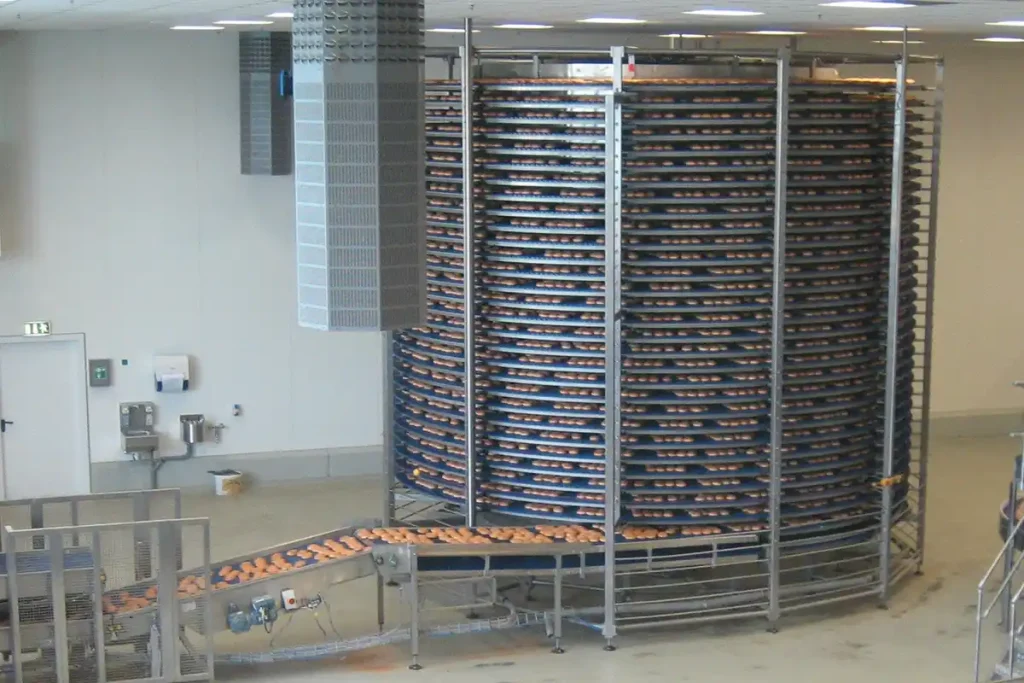
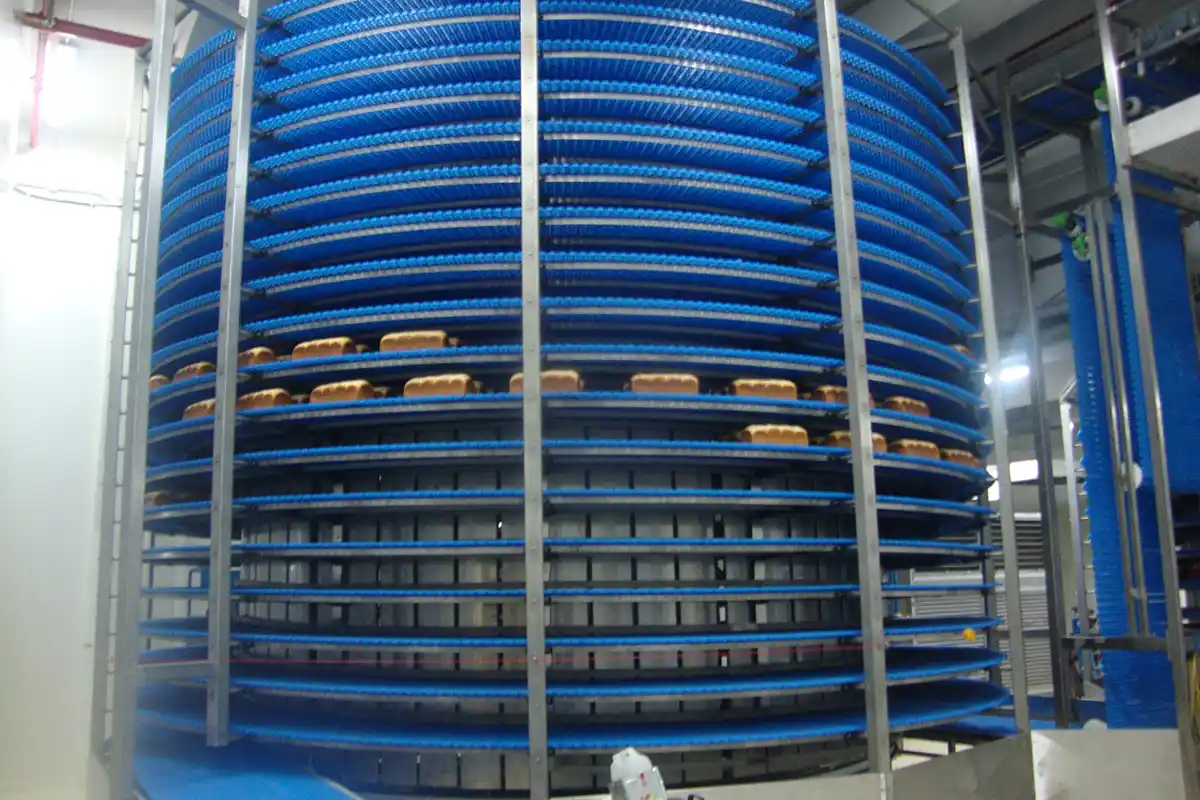
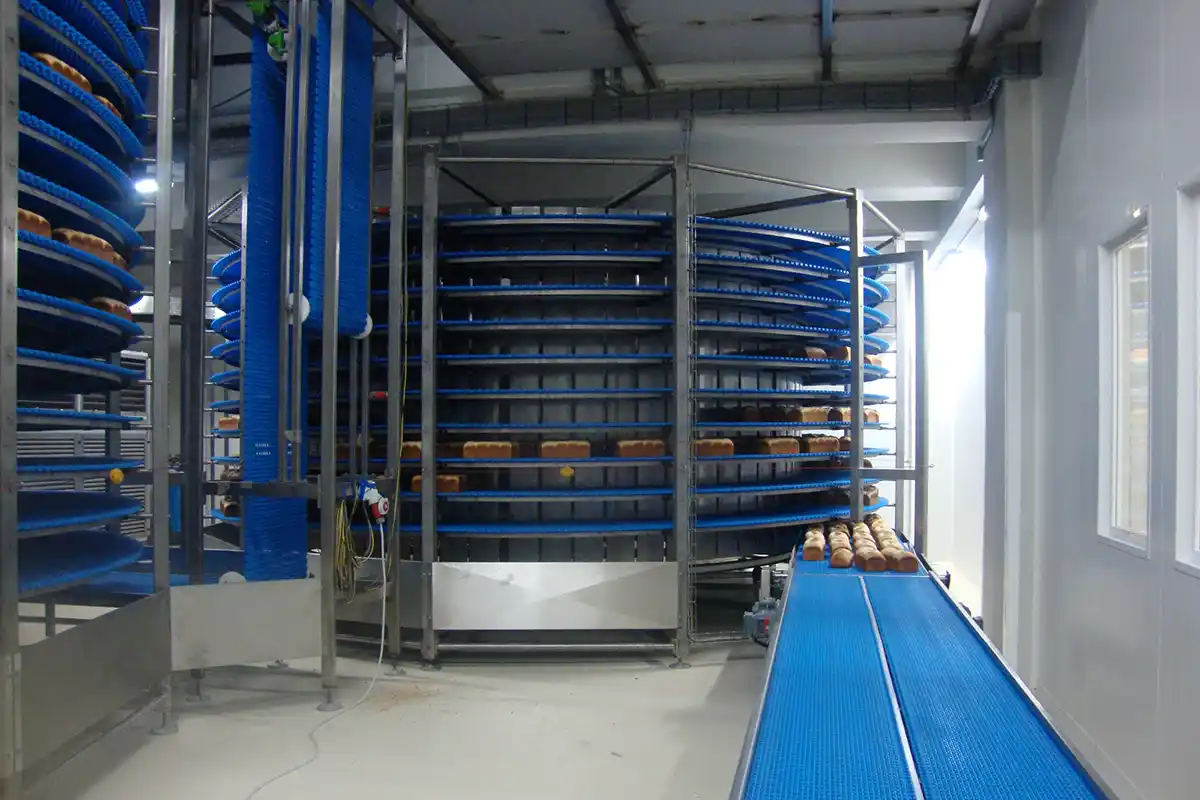
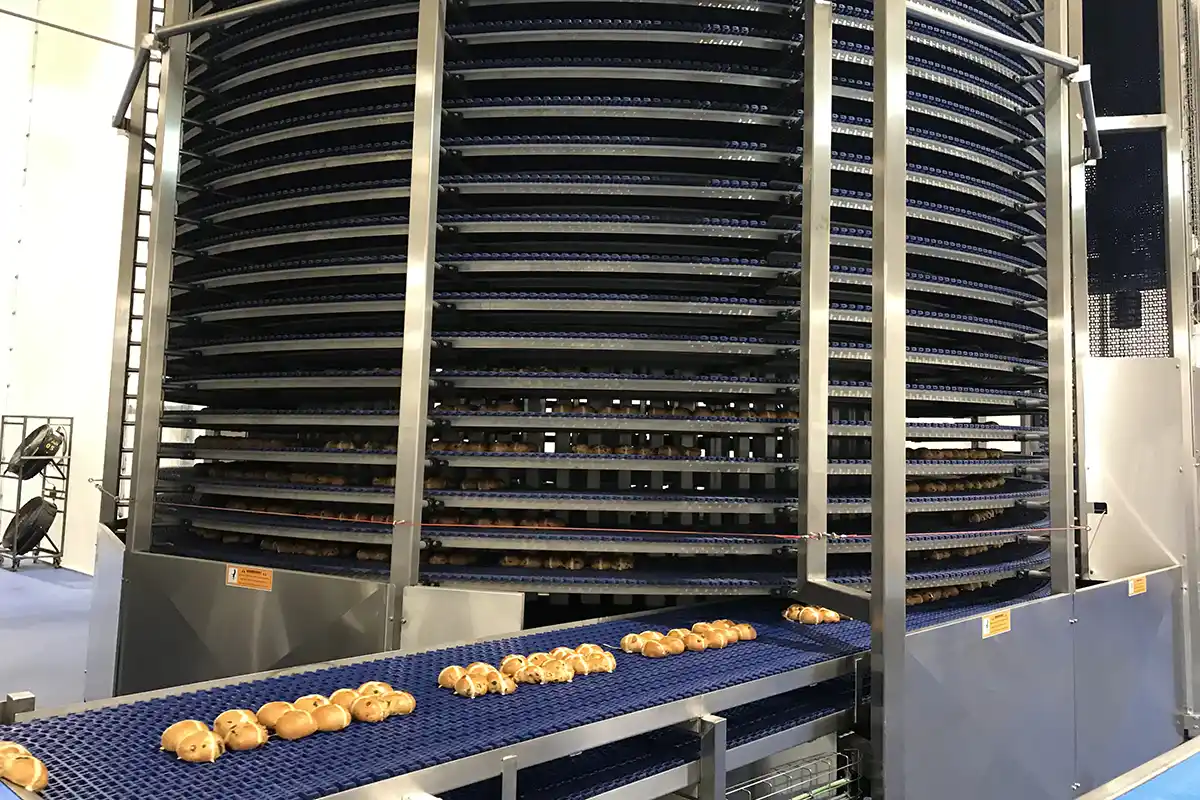
GBS Automation delivers advanced hygienic spiral conveyor systems engineered for maximum performance, reliability, and efficiency in demanding food processing and industrial manufacturing environments.
Our robust spiral solutions are designed to optimize production flow while maintaining the highest standards of hygiene, safety, and operational excellence.
At the heart of every GBS Automation spiral is state-of-the-art control technology that provides precise system management and enhanced production visibility. Recipe-driven product parameters allow operators to quickly configure and switch between products, ensuring consistent processing results while reducing setup times and improving overall productivity.
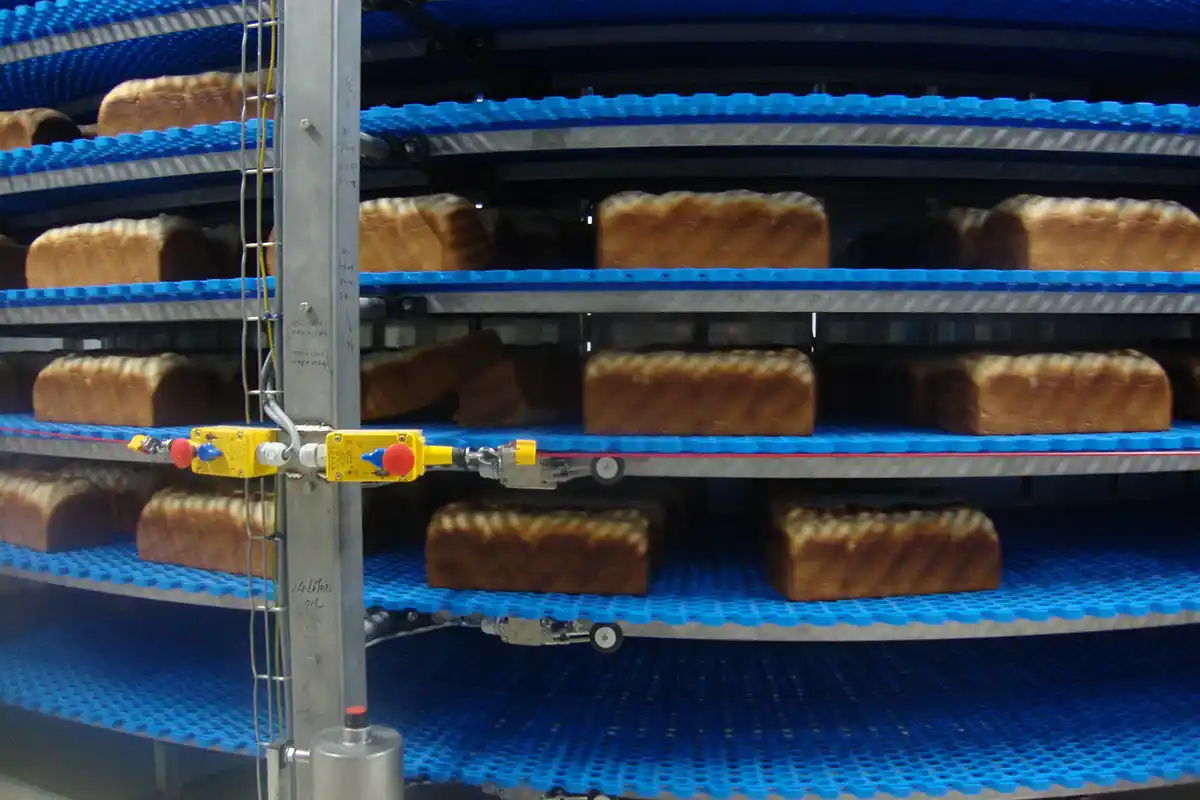
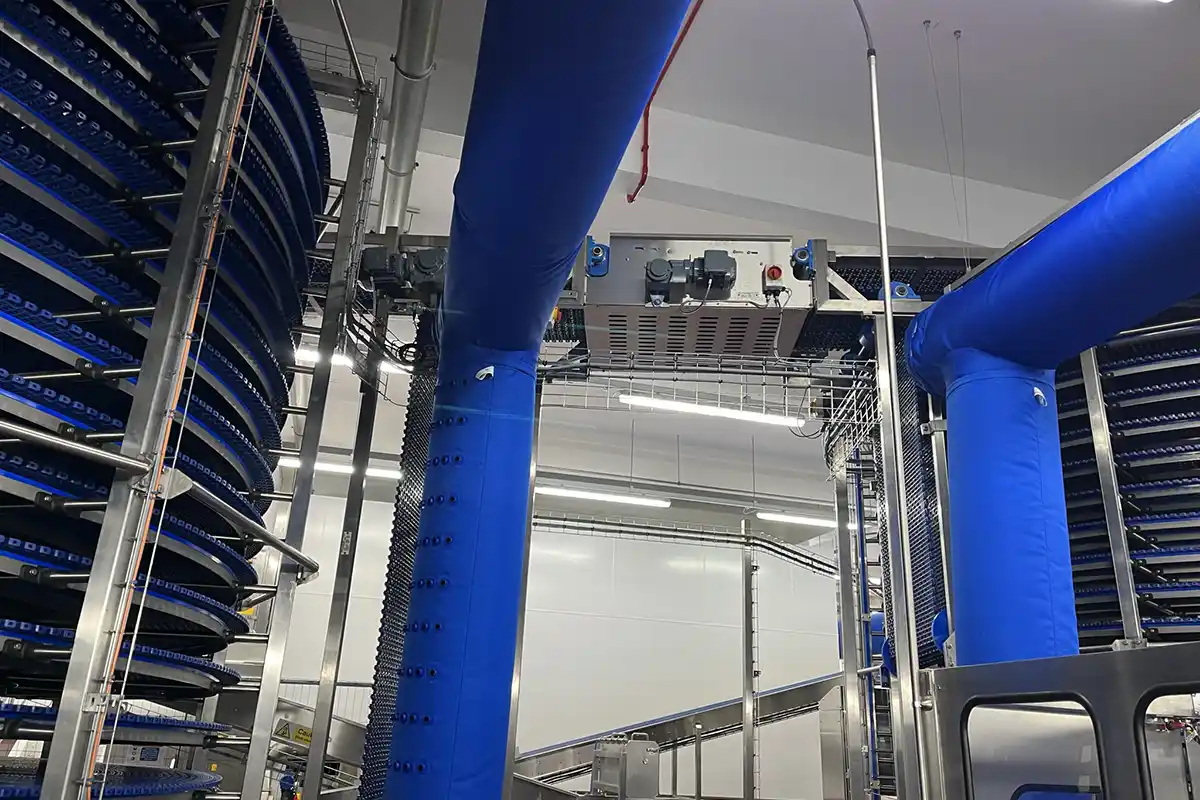
Our spirals feature innovative Intralox DirectDrive™ Technology, eliminating many of the maintenance challenges associated with traditional conveyor drive systems. This proven technology delivers smooth, reliable operation, reduced downtime, and increased system longevity. Additionally, the unique gearbox removal system enables faster servicing and maintenance, minimizing production interruptions and reducing labour costs.
Designed with energy efficiency in mind, GBS Automation spirals incorporate intelligent energy-saving controls that automatically optimize power consumption based on operational requirements. This helps manufacturers reduce energy costs while supporting sustainability goals.
With a strong focus on delivering a low total cost of ownership, our spiral conveyor systems are built for durability, reliability, and long-term performance. Customers benefit from reduced maintenance requirements, lower operating costs, and increased equipment uptime.
GBS Automation offers both ambient air and conditioned air spiral solutions to meet a wide range of cooling, holding, proofing, and product-handling applications. Whether your facility requires standard processing conditions or controlled temperature environments, our systems can be tailored to your specific operational needs.
To further support customers, we provide remote support, system monitoring, and diagnostic capabilities, enabling rapid troubleshooting, proactive maintenance, and improved equipment performance. This ensures your spiral conveyor system continues to operate at peak efficiency while maximizing productivity and return on investment.